Tighter Is Not Always Better: Rethinking Tolerance Specifications as a Strategic Business Decision
Across American manufacturing floors, a persistent belief has shaped engineering decisions for generations: tighter tolerances signal better quality. It is an intuition reinforced by decades of precision culture, customer expectations, and competitive posturing. The tighter the spec, the more serious the manufacturer. The closer the fit, the more capable the operation.
But that assumption deserves serious scrutiny — because in a growing number of documented cases, it is quietly costing manufacturers millions.
The Misalignment Nobody Talks About
Every manufactured component exists within a broader system. A machined shaft connects to a bearing. A housing accepts an insert. A precision-bored cylinder interfaces with a piston assembly. Each of these relationships has a functional requirement — a range within which the assembly performs as intended. That range is defined by physics, by application demands, and by the downstream process that receives the part.
The problem arises when the tolerance specified on the drawing bears little relationship to what the downstream process actually requires. Engineers, often working conservatively or referencing legacy specifications, apply tolerances tighter than the application demands. The result is a part that is technically impressive but practically over-engineered — manufactured to a standard the end use will never test.
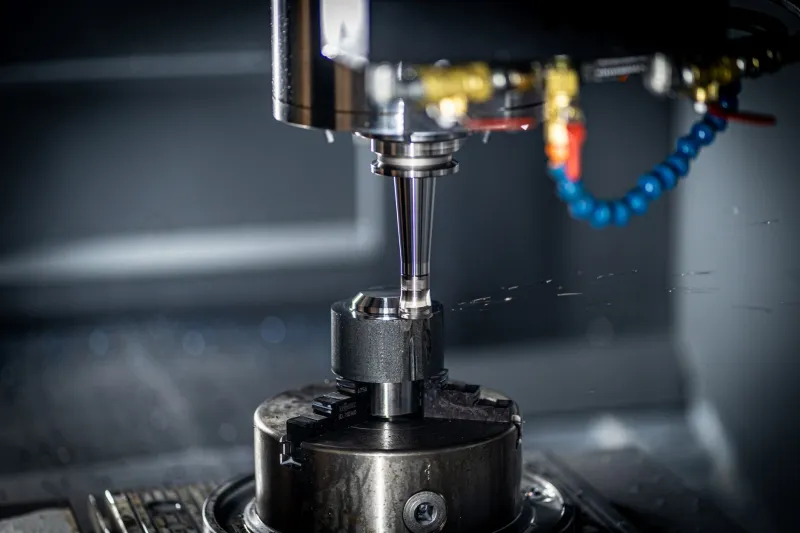
This misalignment is not a minor inefficiency. It compounds across every stage of production. Tighter tolerances demand slower cycle times, more frequent tool changes, greater inspection frequency, higher scrap rates, and more expensive equipment utilization. When multiplied across thousands of parts per production run, the financial impact is substantial.
A Case Study in Strategic Relaxation
Consider a mid-sized contract manufacturer in the Midwest supplying precision housings to an industrial equipment OEM. For years, the housings were machined to a bore tolerance of ±0.0005 inches — a specification inherited from the original design documentation and never revisited. Scrap rates hovered near 8 percent. Cycle times were constrained by the need for multiple finishing passes. Inspection bottlenecks delayed shipment regularly.
A formal tolerance audit, conducted in collaboration with the OEM's engineering team, revealed that the functional assembly requirement — accounting for thermal expansion, operational vibration, and bearing clearance — was fully satisfied at ±0.002 inches. The tighter specification had been carried forward through multiple design revisions without ever being validated against actual performance data.
After controlled testing confirmed that the relaxed tolerance met all functional criteria, the specification was revised. Scrap rates dropped to under 2 percent. Cycle times decreased by approximately 18 percent. Inspection throughput improved measurably. The OEM's field performance data, tracked over the following 18 months, showed no degradation in product reliability.
The tighter tolerance had never been delivering better performance. It had only been delivering higher cost.
Where Over-Specification Originates
Understanding why manufacturers over-specify tolerances requires an honest look at the organizational dynamics that produce engineering documentation.
First, there is the inheritance problem. Many tolerance specifications originate in early design iterations and are carried forward without review. As products evolve, as materials change, and as manufacturing processes improve, the original rationale for a given tolerance is rarely revisited. The specification persists because questioning it requires effort and carries perceived risk.
Second, there is the liability posture. Engineers and quality teams often tighten tolerances as a form of institutional risk management. If a tighter spec is held, any failure is easier to attribute to assembly or application factors rather than the component itself. This creates a culture where precision is used as organizational cover rather than as a functional requirement.
Third, there is the customer expectation dynamic. In competitive bidding environments, manufacturers sometimes specify tight tolerances to signal capability — a marketing function masquerading as an engineering function. The tolerance becomes a credential rather than a constraint.
None of these motivations are rooted in functional necessity. And all of them carry real cost.
The Cascading Effect on Quality Systems
Over-specified tolerances do not merely increase machining costs in isolation. They reshape the entire quality infrastructure surrounding a part.
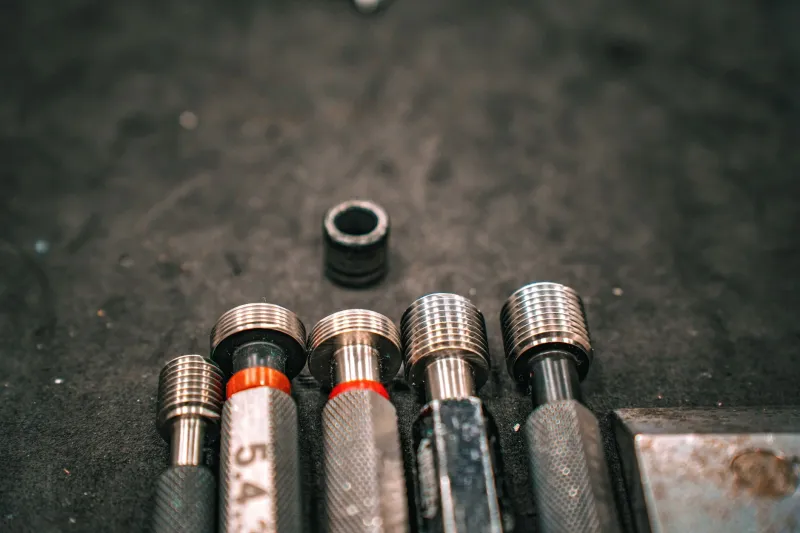
Inspection plans are built around the tightest dimensions on a drawing. When those dimensions are tighter than necessary, inspection protocols become more intensive, more time-consuming, and more expensive than the actual risk profile of the component warrants. Coordinate measuring machines are tied up on parts that could be verified with simpler gauging. Skilled metrology personnel are allocated to measurements that do not meaningfully protect product quality.
Furthermore, supplier qualification criteria are often anchored to the tightest tolerances in a component family. A supplier capable of meeting 95 percent of a part's requirements may be disqualified because of a single over-specified feature — narrowing the supply base unnecessarily and increasing procurement risk.
The quality system, in effect, becomes organized around a fiction: that the tightest tolerance is always the most important tolerance. In reality, the most important tolerance is the one most directly tied to functional performance.
A Framework for Tolerance Rationalization
Addressing over-specification requires a structured approach rather than ad hoc revision. The following framework has proven effective across a range of US manufacturing environments:
Functional decomposition. For each tolerance under review, identify the specific performance requirement it is intended to support. If that requirement cannot be articulated clearly, the tolerance should be flagged for validation.
Stack-up analysis. Evaluate how individual tolerances interact within the full assembly. Tolerances that appear conservative in isolation may be appropriately tight when assembly variation is considered — or they may reveal redundancy that can be safely reduced.
Process capability alignment. Compare the specified tolerance to the demonstrated capability of the manufacturing process. A tolerance that consistently pushes a process to the edge of its capability range is a strong candidate for review.
Field performance correlation. Where field data exists, correlate component tolerance history with reliability outcomes. Parts that have performed well across a range of actual dimensional variation provide empirical evidence for tolerance relaxation.
Controlled validation. Before implementing revised tolerances in production, prototype quantities should be produced, assembled, and tested under representative conditions. Documentation of the validation process protects all parties if the specification change is later questioned.
Precision as a Resource, Not a Default
The broader lesson embedded in tolerance rationalization is one that applies to manufacturing strategy at every level: precision is a resource, and like all resources, it should be deployed where it delivers measurable value.
At Sohar Industries SPC, this principle shapes how technical engagements are structured. Precision is not an end in itself — it is a capability applied in service of functional outcomes, cost efficiency, and long-term product performance. When a tighter tolerance genuinely protects a critical fit or function, it is fully warranted. When it does not, it represents an unnecessary burden on the entire production system.
The manufacturers best positioned to compete in today's US industrial landscape are not those who specify the tightest tolerances. They are those who specify the right tolerances — and who have the analytical discipline to know the difference.
Rethinking tolerance philosophy is not a compromise on quality. It is, in fact, one of the more sophisticated quality decisions a manufacturing organization can make.