Documented but Not Dependable: The Dangerous Gap Between Component Traceability and Verified Material Integrity
There is a particular kind of confidence that comes from holding a thick folder of supplier documentation. Mill certifications, certificate of conformance records, heat numbers, lot codes, chain-of-custody logs — the paper trail feels like proof. For procurement teams and quality managers operating under intense pressure to demonstrate supply chain control, that documentation provides something close to institutional comfort.
But comfort and certainty are not the same thing. And in precision manufacturing environments, that distinction can be extraordinarily costly.
The hard reality is this: knowing precisely where a component came from does not guarantee that the component arriving at your assembly line is still the same material that left the mill, the foundry, or the certified supplier facility. The traceability record documents a moment in time. It says nothing about everything that happened between that moment and the present one.
What Traceability Actually Measures — and What It Doesn't
Supply chain traceability, at its core, is a documentation discipline. It answers the question: where did this come from? It records origins, certifications, lot assignments, and handling handoffs. Done well, it creates an auditable chain that satisfies regulatory requirements, supports quality system compliance, and enables rapid response when defects are discovered.
What it does not do — and what many manufacturers implicitly assume it does — is confirm the current physical state of the material.
A batch of aerospace-grade aluminum alloy certified to precise chemical composition tolerances at the mill is still documented as meeting those tolerances six months later, regardless of how it was stored, shipped, or handled in the interim. The certification does not expire. The material, however, can change in ways that no certificate will ever reflect.
This is the traceability illusion: the belief that a verified origin implies a verified condition.
The Mechanisms of Silent Degradation
Several distinct failure pathways can compromise material integrity between certification and use — none of which leave a mark on any traceability document.
Metallurgical Degradation Through Thermal Cycling
Certain alloys, particularly those used in high-stress aerospace, defense, and energy applications, are sensitive to temperature excursions during transit and storage. Repeated thermal cycling — even within ranges that might appear acceptable — can alter grain structure, affect hardness profiles, or initiate micro-cracking at the surface or subsurface level. A component may look identical to specification under visual inspection and still exhibit fundamentally different mechanical behavior under load.
Hydrogen Embrittlement in High-Strength Steels
High-strength steel fasteners and structural components are particularly vulnerable to hydrogen embrittlement — a condition that can develop during certain electroplating processes or through exposure to hydrogen-generating environments during storage. The degradation is invisible to the naked eye and may not manifest until the component is placed under tensile stress in service. Lot certifications issued prior to plating or storage provide no indication of this risk.
Environmental Exposure and Surface Contamination
Precision components intended for tight-tolerance assembly are frequently compromised by environmental exposure that falls well outside what any traceability record would flag. Humidity-induced oxidation on mating surfaces, particulate contamination from inadequately controlled warehouse environments, and subtle corrosion from proximity to incompatible materials during storage all represent conditions that can degrade functional performance without triggering any documentation alert.
Handling Damage Below Visual Detection Thresholds
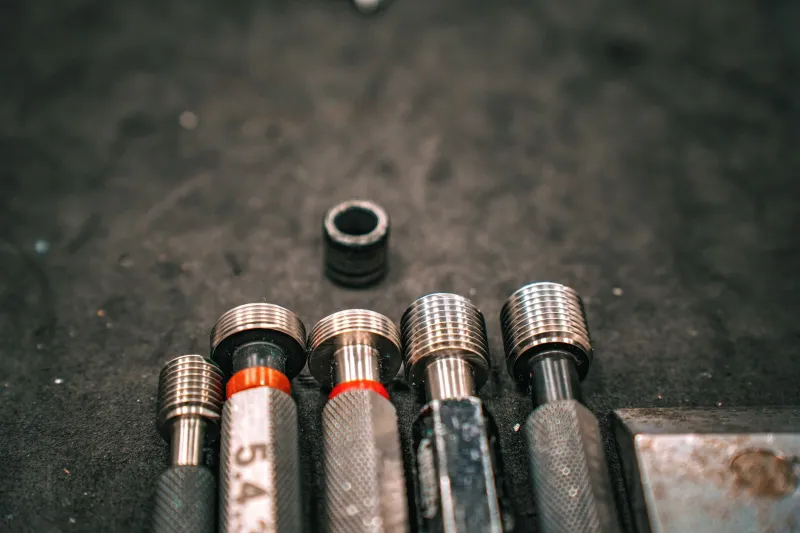
Physical handling across multiple logistics handoffs introduces cumulative mechanical stress that standard incoming inspection protocols frequently miss. Subsurface impact damage to precision-ground surfaces, micro-deformation in threaded features, and edge chipping on hardened components may all remain below the detection threshold of visual and dimensional inspection while still affecting assembly fit, torque performance, or fatigue life.
Why Standard Incoming Inspection Falls Short
Most US manufacturers rely on some form of incoming inspection as the quality gate between the supply chain and the production floor. For many operations, this consists of dimensional verification against drawing specifications, visual examination for obvious damage or contamination, and confirmation that accompanying documentation is complete and matches the order.
This approach is not without value. It catches a meaningful percentage of gross nonconformances and provides a documented audit trail. But it is structurally incapable of detecting the failure modes described above.
Dimensional inspection confirms geometry. It does not confirm material properties. Visual inspection identifies surface anomalies that are visible. It does not identify subsurface damage, internal stress states, or microstructural changes. Document review confirms that a certification exists. It does not confirm that the certification still accurately represents the material.
The result is a quality gate that is wide open to the specific failure modes most likely to produce catastrophic downstream consequences — failures that manifest not at incoming inspection, but at assembly, under load, or in field service.
Closing the Gap: What Verified Integrity Actually Requires
Addressing this gap requires manufacturers to extend their quality thinking beyond documentation and into physical verification — selectively, intelligently, and proportionate to risk.
For critical applications, incoming material verification should include periodic mechanical testing drawn from accepted lots, not merely reliance on mill certifications. Hardness testing, tensile sampling on a statistical basis, and surface integrity assessment using non-destructive evaluation methods such as magnetic particle inspection or ultrasonic testing can provide meaningful assurance that documentation alone cannot.
Storage and handling protocols deserve the same engineering rigor applied to production processes. Controlled environments, segregated storage by material family, humidity monitoring, and defined handling procedures with documented accountability are not administrative overhead — they are functional quality controls that protect the investment already made in certified material.
Supplier qualification processes should include evaluation of in-transit and storage controls, not merely production quality systems. A supplier who certifies material accurately at point of manufacture but ships in uncontrolled conditions is not a controlled supplier in any meaningful sense.
Finally, organizations should periodically audit the correlation between their traceability records and their actual nonconformance data. If documented, certified materials are still generating assembly rejections or field failures, the traceability system is functioning as a record-keeping tool but failing as a quality assurance mechanism. That distinction matters enormously.
Documentation as a Starting Point, Not an Endpoint
Traceability is a necessary capability for any serious precision manufacturing operation. The ability to identify the origin of every component, trace it through the supply chain, and respond quickly when problems emerge is a genuine operational and regulatory requirement.
But documentation is a starting point for quality assurance — not its conclusion. The manufacturers who avoid the most costly material-related failures are those who treat the traceability record as the beginning of a verification process rather than its substitute.
Knowing where a part came from is valuable. Knowing that it still performs as specified when it reaches your line is what actually matters on the production floor.