What the Grid Actually Sends You: Putting Power Quality on the Precision Manufacturing Scorecard
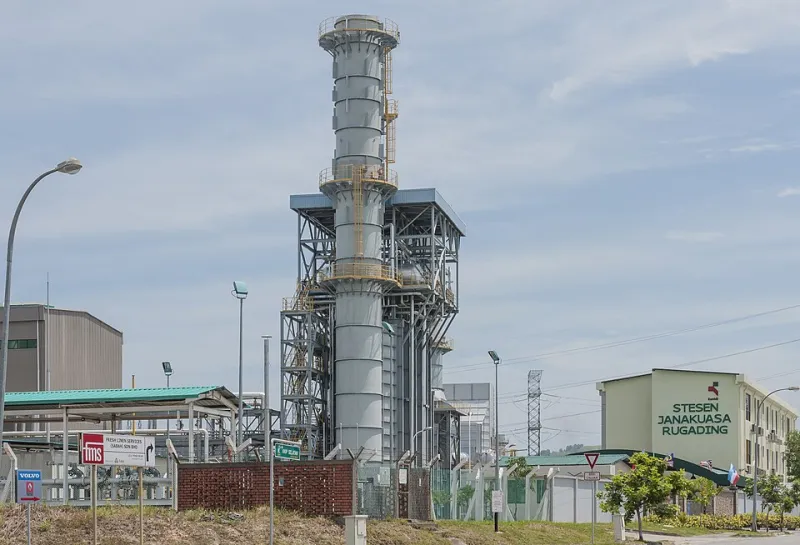
Photo: CEphoto, Uwe Aranas, CC BY-SA 3.0, via Wikimedia Commons
A precision shop will spend six figures on a machine that holds tolerances measured in microns, then plug it into a feeder whose voltage has never been measured at all. That contrast is not a criticism of capital planning. It is simply an observation about where attention tends to go: toward the equipment that makes chips, and away from the invisible commodity that makes the equipment work.
Power quality rarely announces itself with a bang. A utility fault that darkens an entire plant is easy to diagnose, easy to insure against, and easy to remember. The problems that erode throughput tend to be smaller and far more frequent — a sag that lasts four cycles, a harmonic distortion pattern that builds through the afternoon, a transient that resets a drive but leaves no message.
The Failure Mode Nobody Logs
Ask a production manager about the last unplanned stop and the answer is usually specific: a tool broke, a fixture slipped, an operator caught an out-of-tolerance feature. Ask why a batch of parts drifted high on a diameter that had been stable all month and the answer becomes vaguer. Machine drift, material variation, ambient temperature. Power quality rarely makes that list, largely because it is not measured, and what is not measured cannot be blamed.
The practical consequence is a chronic misattribution of cause. Recurring spindle faults get explained as a tired drive. Servo alarms get written off as nuisance codes. Measurement systems that pass calibration yet disagree between shifts get attributed to operator technique. Each of these may have an electrical origin, but without data the diagnosis defaults to the nearest familiar explanation.
What Power Quality Actually Means on a Shop Floor
Voltage sags — brief dips below nominal — are the most consequential anomaly for precision operations. A sag of a few cycles can be enough to drop a contactor, reset a CNC control, or force a variable-frequency drive into a protective trip. Motors restart; the part in the fixture may not survive the interruption, and the rework is rarely charged back to its true cause.
Harmonics present differently. Distortion introduced by non-linear loads accumulates across a facility and manifests as heat: warm neutrals, overloaded transformers, motors that run hotter than their duty cycle should require. On a compressed-air system, which is effectively a plant-wide utility with its own electrical dependencies, harmonic-driven inefficiency shows up as pressure instability at the point of use — and pressure instability, in turn, degrades air-bearing spindles and air gauging that assume a steady supply.
Transients and swells are shorter and less predictable. They may not stop a machine at all, but they can corrupt encoder signals, provoke intermittent communication faults on a network, or leave a controller in an ambiguous state that requires a manual restart nobody records.
The common thread is that each anomaly operates below the threshold of a visible outage while sitting above the threshold that precision processes can absorb.
Reading the Electrical Signature
An audit does not need to begin with a plant-wide investment. It can begin with a power quality analyzer placed at the service entrance for a week or two, and then at the individual distribution panels serving the most tolerance-sensitive equipment. The goal is a baseline: nominal voltage, typical sag frequency and depth, total harmonic distortion by phase, and the presence of neutral current that should not exist.
Placing recorders at the machine level, even briefly, produces a more useful picture than service-entrance data alone. A CNC that trips at a given voltage threshold can be matched against the recorded sag events of the preceding weeks. If the trips line up, the conversation changes from speculation to evidence.
Timestamps matter as much as magnitudes. Correlating electrical events with maintenance logs, scrap reports, and first-article failures is what converts an engineering curiosity into an operational finding.
Quantifying Exposure in Production Terms
Electrical data becomes actionable only when it is translated into the language the business already uses. A shop does not need a harmonic spectrum; it needs to know how many hours of spindle time were lost to events that a ride-through device would have absorbed.
A workable translation has three components. First, count the events: how many disturbances per month exceed the tolerance of the critical equipment. Second, cost each event: scrap value, rework hours, restart labor, and the schedule slippage passed downstream. Third, identify the subset that a specific remedy would eliminate.
That third step is where discipline matters. Not every anomaly justifies a capital response. A shop that installs conditioning on every panel will spend heavily to solve problems that were never costly. The exposure model should point to a small number of circuits where the economics are clear.
A Resilience Plan Proportional to the Risk
Remedies generally fall into three tiers. At the equipment level, ride-through capability on controls, line reactors on drives, and proper grounding and bonding address the most common trip mechanisms. At the distribution level, separating sensitive loads from high-distortion loads on dedicated panels often resolves more than any device purchase. At the facility level, an automatic transfer scheme or a standby generator may be justified — but usually only for specific processes, not for the entire building.
Sequencing these measures by cost-per-event-avoided keeps the plan honest. A grounding audit and a panel separation study frequently deliver more reliability per dollar than a large conditioning installation, and they establish the baseline against which later capital requests can be judged.
Making It a Standing Metric
Power quality belongs on the same dashboard as on-time delivery, first-pass yield, and unplanned downtime — not because electricity is interesting, but because it is an input whose variability propagates directly into output variability. A single number, such as disturbance events exceeding equipment tolerance per month, is enough to keep the topic visible without turning every utility blip into a project.
Precision manufacturing is, at its core, an exercise in controlling inputs. Temperature is controlled. Humidity is controlled. Coolant chemistry is controlled. The electrical supply deserves the same treatment: measured, baselined, and reviewed on a schedule rather than investigated after a bad week.